Time:2026-08-04 Form:本站
How Implant Factories Achieve Micron-Level Accuracy
When a dental implant fails early, the root cause is rarely the titanium itself. More often it hides in a few microns of error at the implant–abutment interface — a gap you cannot see, but bacteria, cyclic load, and your warranty claims certainly can.
That is why "micron-level accuracy" is not marketing language in our industry. It is the difference between a connection that stays sealed for a decade and one that loosens, leaks, or fractures. In this article we break down how implant factories actually reach that accuracy, where microns are quietly lost, and how you can verify a supplier's real capability before you commit to a program.
A micron (µm) is one-thousandth of a millimeter. A human hair is roughly 50–70 µm wide. In implant manufacturing, the tolerances that matter most sit well below that.
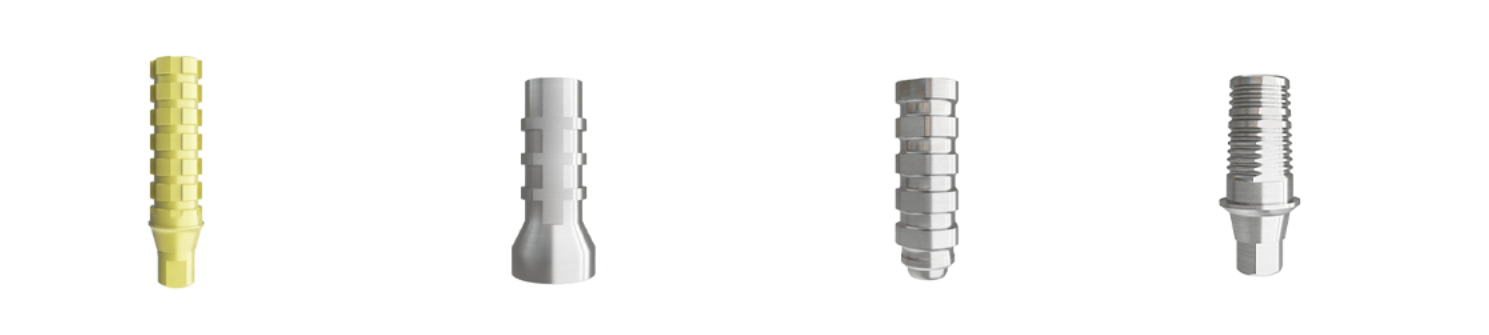
The critical zones are not the visible threads. They are the mating surfaces where the implant meets the abutment and the screw:
Conical / internal connection fit: typically toleranced to ±2–5 µm on diameter and taper angle.
Implant–abutment microgap: a well-made connection targets a marginal gap below 5 µm, and premium conical systems aim for 1–3 µm.
Thread pitch and flank position: controlled to a few microns to keep insertion torque predictable.
Prosthetic platform flatness: deviations here translate directly into screw preload loss.
Here is the part most articles skip: accuracy is meaningless without repeatability. Hitting ±3 µm once is luck. Hitting it on unit 1 and unit 50,000 is manufacturing capability. Buyers should always ask about the second number, not the first.
Experienced manufacturers think in terms of a tolerance stack-up — an error budget. Every step spends part of it. If the total spend exceeds the design tolerance, the part fails inspection no matter how good any single stage was.
| Stage | Typical error contribution | What controls it |
|---|---|---|
| Raw bar stock (roundness, cleanliness) | 3–10 µm | Material grade, mill certification, inclusion control |
| Thermal drift during machining | 2–8 µm | Coolant strategy, machine warm-up, shop climate control |
| Tool wear over a production run | 2–6 µm | Tool-life monitoring, in-process compensation |
| Workholding / re-fixturing | 3–10 µm | Single-setup machining, collet quality |
| Measurement uncertainty | 1–3 µm | Calibrated CMM, environment, gauge R&R |
Notice that the raw material and the fixturing often cost more microns than the cutting itself. This is why a factory that only talks about its CNC brand is telling you half the story. The disciplined ones talk about their whole error budget.
You cannot machine precision into a bar that arrives inconsistent. Titanium for dental implants is usually commercially pure Grade 4 ( Ti, ASTM F67) for fixtures, and Ti-6Al-4V Grade 5 or the ELI Grade 23 (ASTM F136) for abutments and multi-unit components.
The grade choice is a real engineering trade-off, not a preference:
| Property | Grade 4 Ti | Ti-6Al-4V (Grade 5) | Ti-6Al-4V ELI (Grade 23) |
|---|---|---|---|
| Yield strength | ~480–655 MPa | ~800–900 MPa | ~795–875 MPa |
| Fatigue behavior | Good | High | Highest (low interstitials) |
| Biocompatibility | Excellent (no alloying) | Excellent | Excellent, ELI-grade purity |
| Typical use | Implant fixtures | Abutments, screws | Long-term load-bearing parts |
| Machinability | Easier, more ductile | Harder, work-hardens | Similar to Grade 5 |
For micron work, what matters as much as the grade is lot-to-lot consistency: tight control of oxygen content, low inclusion levels, and stable hardness. A batch that swings in hardness forces your tools to cut differently part to part — and that variation lands straight in the microgap.
This is one practical reason we standardize our fixture and abutment blanks on traceable Grade 4 CP Ti and Grade 23 ELI stock at RE-TECH: every lot ships with a mill certificate covering chemistry and mechanical properties, so the machining parameters we validated on lot A still hold on lot Z. If a supplier cannot hand you that certificate, you are absorbing their material risk into your finished device.
Titanium is a difficult metal to machine precisely, for reasons that directly threaten accuracy:
Low thermal conductivity. Heat concentrates at the cutting edge instead of dissipating, causing local expansion and dimensional drift. High-pressure through-tool coolant is not a luxury here; it is a tolerance-control tool.
Work hardening. Titanium hardens where it has just been cut, so dull tools or the wrong feed rate leave an uneven surface that no polishing step can fully correct.
Elastic springback. The material flexes under tool pressure and springs back after, so the measured cut is not the commanded cut unless the process compensates.
Serious implant factories answer these with a combination of methods:
Swiss-type (sliding-head) CNC lathes for small, slender parts like implant fixtures — the guide bushing supports the bar right at the cutting zone, minimizing deflection.
5-axis machining for complex abutment geometries in a single setup, eliminating the re-fixturing errors from the table above.
In-process tool compensation, where the machine measures and adjusts for tool wear mid-run rather than waiting for a bad batch.
| Approach | Best for | Accuracy strength | Trade-off |
|---|---|---|---|
| Swiss-type CNC | Slender fixtures, screws | Minimal deflection, tight diameters | Less suited to complex 3D forms |
| 5-axis CNC | Angled/custom abutments | Single-setup, no re-fixturing error | Higher programming skill needed |
| Milling from discs | Multi-unit bars, lab-side parts | Batch flexibility | Needs strong blank consistency |
| Metal additive (DMLS) | Complex lattices, prototypes | Geometric freedom | Post-machining still required for fit surfaces |
A point worth making plainly: additive manufacturing is exciting, but the mating surfaces of an implant connection are still finished by subtractive machining. Microns at the interface are earned by cutting and measuring, not by printing alone.
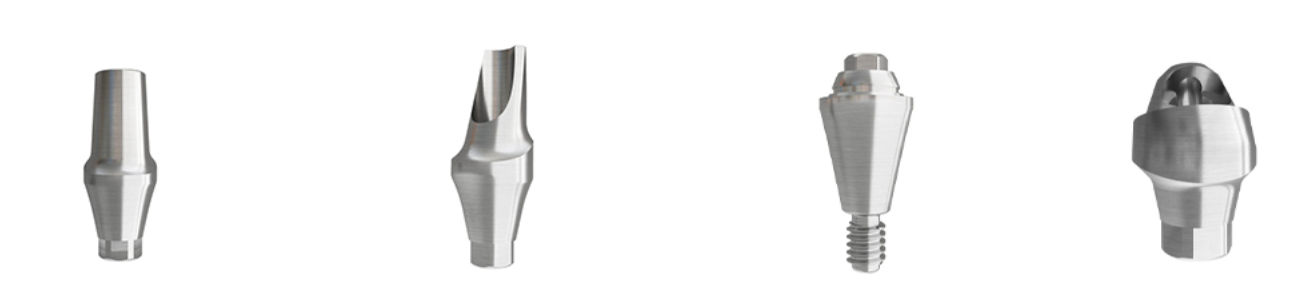
A factory's real accuracy is capped by its measurement system. If your gauge uncertainty is 3 µm, you cannot honestly claim a 2 µm tolerance.
The tools that separate serious manufacturers:
Coordinate Measuring Machines (CMM) in a temperature-controlled room (20 °C ± 1 °C) for interface diameters, tapers, and flatness.
Optical and laser scanners for full-surface deviation maps against the CAD model.
Automated optical inspection for thread integrity and surface defects at production speed.
Just as important is statistical control. Instead of measuring one part per batch, capable factories track process capability indices (Cpk) across the run. A Cpk above 1.33 means the process reliably stays inside tolerance with margin to spare. Ask a potential supplier for their Cpk data on the interface diameter — the answer tells you instantly whether they manage by data or by hope.
Accuracy and surface treatment can fight each other if uncontrolled. Sandblasting and acid etching (SLA) roughen the fixture surface to promote osseointegration — but that roughness must stop precisely at the connection.
Good practice masks the mating surfaces so the microgap you machined is not undone by the finishing line. Anodizing for color-coding abutments adds only a nanometer-scale oxide and does not disturb fit. The discipline is knowing exactly where micron-smooth must meet micro-rough, and controlling that boundary.
If you take one practical thing from this article, make it this list. Send it to any candidate factory:
Material traceability: Do you supply mill certificates (chemistry + mechanical) for every lot of Grade 4 and Grade 23 stock?
Interface tolerance in numbers: What is your toleranced value and measured Cpk on the implant–abutment fit?
Microgap data: Can you show marginal gap measurements on assembled connections?
Metrology environment: Is your CMM temperature-controlled, and what is your gauge R&R?
Single-setup capability: How do you eliminate re-fixturing error on complex abutments?
Validation records: Can you provide process validation (IQ/OQ/PQ) documentation for a regulatory submission?
A supplier who answers these with specifics is managing an error budget. One who answers with brochures is managing a sales pitch. The difference will show up in your field-failure rate.
At RE-TECH, this checklist is essentially how we run the floor: traceable Grade 4 and Grade 23 ELI titanium, single-setup 5-axis and Swiss machining for the fit-critical features, and CMM-based Cpk records we can hand to your regulatory team. We share it here not as a pitch but because these are the questions that protect you regardless of which factory you choose.

1. How precise is a dental implant, really?
The visible threads are machined to standard tolerances, but the implant–abutment connection is typically held to ±2–5 µm, with premium conical systems targeting a marginal microgap of 1–3 µm. That interface, not the outer thread, is where precision matters most.
2. Why does the implant–abutment microgap matter so much?
A gap larger than about 5 µm allows bacterial microleakage and micromovement under chewing load. Over time this drives peri-implant inflammation, screw loosening, and marginal bone loss — the most common causes of late implant complications.
3. Which titanium grade is best for dental implants?
Commercially pure Grade 4 (ASTM F67) is standard for implant fixtures because of its excellent biocompatibility and ductility. Ti-6Al-4V Grade 5 and the higher-purity ELI Grade 23 (ASTM F136) are used for abutments and load-bearing components that need greater strength and fatigue resistance.
4. Is 5-axis CNC or 3D printing better for accuracy?
For the fit-critical mating surfaces, subtractive machining (5-axis and Swiss-type CNC) still leads because it delivers the surface finish and dimensional control the connection needs. Additive manufacturing excels at complex geometry and prototyping, but interface surfaces are usually finish-machined afterward.
5. How can I verify a factory actually holds micron tolerances?
Ask for measured data, not target values: interface Cpk from a CMM, marginal gap measurements on assembled parts, and lot-level mill certificates. Repeatable data across a production run is the real proof of capability.
6. Does surface treatment reduce connection accuracy?
It can if uncontrolled. Reputable manufacturers mask the mating surfaces during sandblasting and acid etching so roughening stays on the fixture body, leaving the machined microgap intact.
7. What tolerance should I specify for a custom abutment program?
Start from the connection system's published fit tolerance (often ±2–5 µm) and require the supplier to demonstrate a Cpk of at least 1.33 on that feature. Specifying capability, not just a number, is what keeps quality stable at volume.